Stock code: 601677
Stock code: 601677
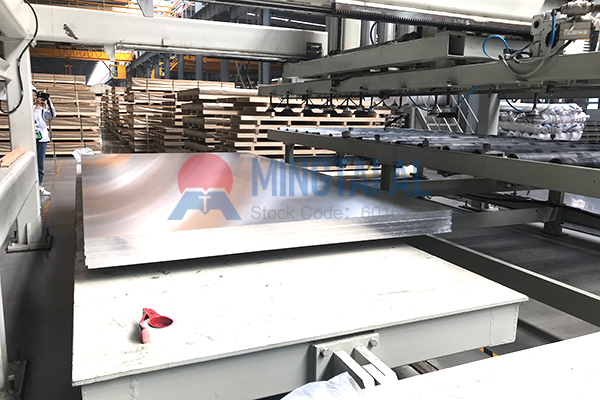
Burrs on cut edges are the most common issue when processing laser cutting aluminum sheet. Removing them after cutting adds extra steps and drives up costs. Many tend to look for solutions in machine settings or gas parameters, but overlook a more fundamental factor—the choice of alloy grade.
The right alloy delivers smooth edges and efficient cutting. The wrong one leads to rough edges and endless rework. So which alloy actually gives you a burr‑free result?
Aluminum is more challenging to cut cleanly than steel, due to its physical properties. It has a high reflectivity to laser beams, meaning only part of the energy is absorbed at the start of cutting. At the same time, aluminum conducts heat extremely well—heat quickly moves away from the cut zone, so molten metal solidifies before the assist gas can blow it away. On top of that, molten aluminum has high surface tension, tending to stick to the bottom of the kerf and form hard burrs when it cools.
These are inherent traits of aluminum and cannot be changed. The key point is that different alloys behave quite differently in melting and solidification, which directly affects edge quality after cutting.
|
Alloy |
Key Trait |
Laser Cutting Performance |
Best For |
|
5052 (5000 Series) |
High stability, wide parameter tolerance |
Clean edges, very few burrs. Performs well even with average equipment. |
Bent panels, enclosures, appearance parts |
|
6061 (6000 Series) |
High strength, good edge quality |
Clean edges, but T6 temper requires precise speed/power control. |
Structural parts, precision components |
|
1060/1100 (Pure Aluminum) |
Highest reflectivity |
Low energy coupling, risk of lens damage. Edge quality inconsistent. |
Special purity requirements only |
|
3003 (3000 Series) |
Soft, prone to heat distortion |
Thin sheets (under 1mm) easily warp and stick slag. Demanding to process. |
Thin-gauge applications with careful parameter control |
|
7075 (7000 Series) |
Ultra-high strength |
Fine burrs common along edges. Not recommended if edge quality is priority. |
Applications where extreme strength is mandatory |
Key takeaway: 5052 and 6061 are the top choices for laser cutting aluminum. The decision between them comes down to balancing strength requirements against process controllability.
With the right alloy, proper process parameters can then deliver their full benefit. The following factors are equally important, but they are adjustable variables at the processing stage:
– Assist gas – high‑purity nitrogen with sufficient pressure, otherwise molten metal cannot be effectively removed.
– Focal point position – a “negative focus” setting is often used, creating a wider kerf bottom for easier slag removal.
– Cutting speed – too fast leads to incomplete cuts, too slow increases burrs. Settings must be adjusted for each alloy and thickness.
It is worth noting that a well‑chosen alloy significantly reduces the need for post‑cut edge treatment. This has nothing to do with whether the supplier offers surface finishing or additional processing—it is determined by the material itself.
If you are selecting laser cutting aluminum sheet, the following approach may help:
Define the end use first – For bent panels, prioritize 5052; for load‑bearing structures, choose 6061.
Tell your supplier about the cutting method – Laser cutting has specific requirements for flatness and internal stress. Different applications call for different stress control standards.
Pay attention to temper – T6 temper is harder but more heat‑sensitive. If your equipment has limited adjustment capability, O or H tempers can be easier to process.
Test small samples on your own equipment – Compare burr rate, scrap rate, and downstream finishing costs for different alloys. This is the most reliable way to make a decision.
Look at total cost, not unit price – A cheaper alloy may produce more burrs and higher scrap, making the overall cost significantly higher.
Choosing the right alloy gives you clean cut edges from the very beginning, saving unnecessary work downstream.
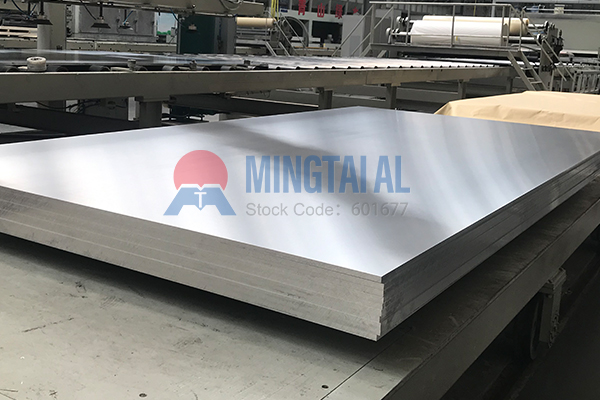
Mingtai Aluminum offers a full range of high‑quality aluminum sheet for laser cutting, including 5052 and 6061, providing a solid foundation for your production.
Q: Which aluminum alloy gives the fewest burrs in laser cutting?
A: 5052 cuts stably with very few burrs, making it a strong choice for laser cutting.
Q: Which is better for laser cutting, 6061 or 5052?
A: 5052 offers wider process tolerance and is easier to handle; 6061 has higher strength but needs tighter parameter control.
Q: Are burrs always a material problem?
A: Multiple factors are usually involved, but the right alloy greatly reduces burr risk.
Q: Is pure aluminum suitable for laser cutting?
A: It can be cut, but high reflectivity and demanding equipment requirements make it less practical than 5052 or 6061.
Q: What assist gas is used for laser cutting aluminum?
A: High‑purity nitrogen at sufficient pressure to blow molten metal out of the kerf.